Nylon 6 so với Nylon 66
PA6 vs PA66: the quick engineering answer
Choose PA6 first when processing economy, toughness and broad general-purpose use lead the decision. Choose PA66 first when higher melting temperature, stiffness retention and heat performance justify tighter drying and processing control.
PA6 vs PA66 property comparison
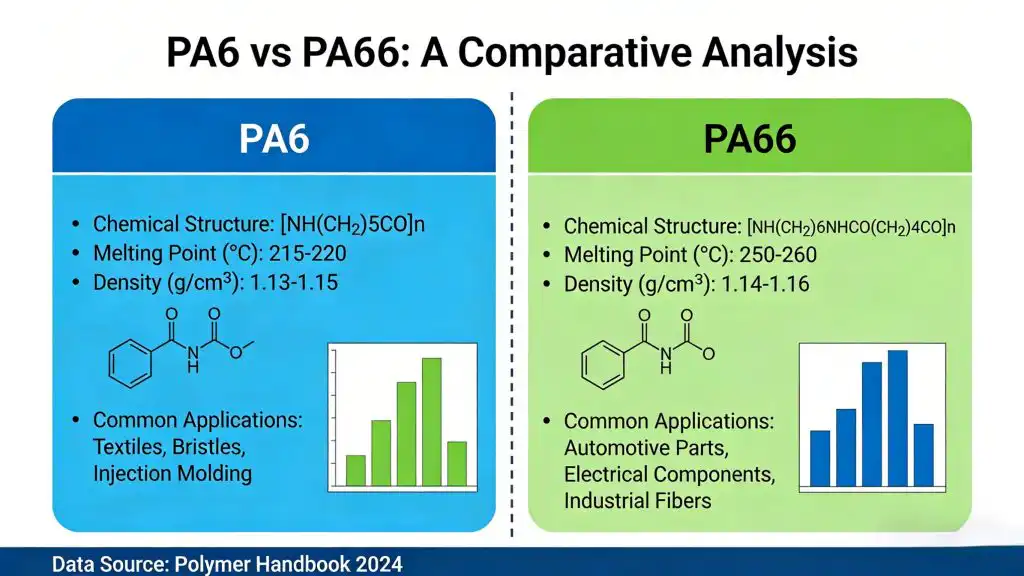
PA6 (nylon 6) and PA66 (nylon 66 or nylon 6/6) are both engineering polyamides. Their chemistry changes melting behavior, crystallization, moisture response and processing. The figures below are typical reference values for unfilled grades; they are not a substitute for the datasheet of the grade used in production.
| Selection factor | PA6 (Nylon 6) | PA66 (Nylon 66) | What it means for the part |
|---|---|---|---|
| Melting point | About 220–225°C | About 255–265°C | PA66 usually provides more thermal margin; actual service temperature depends on grade, load and aging. |
| Dry tensile strength | Commonly around 70–85 MPa | Commonly around 75–90 MPa | The ranges overlap. Reinforcement and moisture conditioning can matter more than the base polymer name. |
| Dry tensile modulus | Commonly around 2.4–3.2 GPa | Commonly around 2.7–3.5 GPa | PA66 is often the stiffer dry material, but both soften as moisture content increases. |
| Phản ứng với độ ẩm | Hygroscopic | Hygroscopic | Compare dry and conditioned data, then define conditioning and dimensional inspection in the drawing or control plan. |
| Processing | Lower melt temperature and generally wider processing economy | Higher melt temperature and tighter thermal control | Both need correct drying. Residence time, mold temperature and moisture must match the grade datasheet. |
| Typical positioning | General mechanical parts, housings, gears and cost-sensitive molded components | Heat-exposed housings, connectors, structural parts and reinforced grades | Use the operating condition and part geometry to decide, not the material name alone. |
How to choose between PA6 and PA66
Choose PA6 when
- Part cost and processing efficiency are primary constraints.
- Good toughness, wear resistance and general mechanical performance are sufficient.
- The working temperature does not require PA66’s additional thermal margin.
- A PA6 GF grade already meets the dimensional and structural targets.
Choose PA66 when
- The part needs higher dry stiffness or strength retention at elevated temperature.
- Connectors, brackets or under-hood parts face heat and sustained mechanical load.
- A validated PA66 GF, FR, heat-stabilized or impact-modified grade matches the approval requirements.
- The molding process can control drying, melt temperature and crystallization consistently.
PA6 vs PA66 for common application requirements
| Yêu cầu | Bắt đầu với | Approval check |
|---|---|---|
| Cost-sensitive housing or general mechanical part | PA6 | Impact, stiffness, dimensional tolerance and humidity exposure. |
| Heat-exposed structural or electrical component | PA66 | Continuous and peak temperature, load, aging, flame rating and electrical requirement. |
| High stiffness or low creep | PA6 GF or PA66 GF | Glass content, fiber orientation, weld lines, warpage and conditioned properties. |
| Flame-retardant component | Exact PA6 FR or PA66 FR grade | Required rating, thickness, color and applicable certification for the named grade. |
| Precision part exposed to humidity | Compare conditioned PA6 and PA66 data | Equilibrium moisture, tolerance stack, conditioning method and inspection timing. |
Processing and mold-design differences
PA66 generally runs at a higher melt temperature than PA6. Both materials are moisture-sensitive before molding, so drying should follow the exact supplier datasheet and be checked with suitable moisture-control procedures. Poor drying can cause splay, hydrolytic degradation and loss of mechanical performance.
- Dụng cụ: allow for grade-specific shrinkage and anisotropy, especially with glass fiber.
- Temperature control: use the supplier’s melt and mold-temperature window; avoid applying a generic nylon setting to every grade.
- Inspection: define whether dimensions are checked dry, after conditioning or after environmental exposure.
- Regrind and residence time: agree the limits before qualification when mechanical or appearance consistency is critical.
PA66 grades and real datasheet evidence
PA66 GF10, GF15, GF20, GF25, GF30, GF35, GF40 and GF50 are separate formulations. Flame-retardant versions are also listed separately. Do not copy a GF30 value into an unfilled, GF50 or GF30 FR specification.
For PA66 material selection
Use the PA66 properties and grades guide to define the base resin, reinforcement and operating condition.
For PA66 GF30
Xem lại PA66 GF30 Datasheet in the verified download library, then request the exact grade document and applicable certificate with the quotation.
The available project documentation can include the grade datasheet, a batch-specific certificate of analysis, and applicable RoHS, REACH or UL documentation where the selected grade and project require it.
PA6 vs PA66 FAQ
Is PA66 always stronger than PA6?
No. PA66 often has higher dry stiffness and heat capability, but grade formulation, reinforcement, moisture condition, temperature and part design can reverse a simple material-family comparison.
Which absorbs more moisture, PA6 or PA66?
Both are hygroscopic. Published values depend on test method, exposure and conditioning state, so compare the exact grades under the same test conditions and design around in-use moisture.
Can PA6 GF30 replace PA66 GF30?
Sometimes, but not by name alone. Compare tensile and flexural data, heat aging, impact, shrinkage, moisture response, flame rating, surface requirements and the molded part test.
What should I send for a material review?
Send the drawing or CAD, load, working temperature, humidity or chemical exposure, tolerance, annual volume, color, required certifications and any currently approved material.
Related PA66 and nylon engineering guides
- What is PA66? Properties, grades and applications
- PA66 GF30 material guide
- Nylon moisture absorption and dimensional effects
- Dịch vụ ép phun nylon
- PA6 vs PA66 vs PA12 comparison
Request a PA6 vs PA66 Material and Part Review
Send the information that changes the decision. The technical team can match the resin family, reinforcement and manufacturing route before quotation.
Drawing or CAD, critical dimensions and tolerance.
Load, temperature, humidity and chemical exposure.
PA6 or PA66, reinforcement, color and required documents.
Prototype or production quantity, destination and target timing.